On 16 October 2026, Indonesia's Ministry of Industry highlighted the growth opportunity in electronics and electrical components. Citing McKinsey Global Institute, the ministry said the global electronics-components market could exceed US$1 trillion by 2030, driven partly by electric vehicles, AI and the Internet of Things.
Indonesia already has meaningful capability.
Domestic SMEs are producing printed circuit board assemblies, wire harnesses, connectors, copper braid, electrical panels and power-protection and distribution systems.
But the ability to manufacture components does not mean every design is production-ready.
That is where Design for Manufacturing begins.
CAD Completion Is Not Product Completion
In a linear development process, engineering finishes the design and passes the file to manufacturing.
The factory then produces it.
Reality is less clean.
Design decisions already determine material selection, tolerances, fabrication methods, component placement, assembly sequence, test access and tooling requirements.
ASME describes Design for Manufacturing as designing products for economical production without sacrificing function and performance, while considering material availability, tooling, tolerances, testing and collaboration with manufacturing engineers.
The question therefore is not only:
“Does the design work?”
It is:
“Can we repeatedly build and verify it under real manufacturing conditions?”
Manufacturing Knowledge Needs to Arrive Earlier
NIST work on integrating process planning with conceptual design notes that major manufacturing-cost consequences are committed during specification and design. Manufacturability and cost therefore need to be assessed as early as practical in development.
ASME describes the old model as throwing designs “over the wall” to manufacturing.
That approach creates expensive late discoveries: non-standard components can require retooling, material choices can delay production, and redesign becomes progressively more costly as the project advances.
DFM brings production knowledge to the other side of that wall before the design becomes expensive to change.
“Possible to Build” Is Not Enough
A skilled technician can often build a prototype once.
Commercial production asks a different question.
Can the same result be achieved repeatedly?
Are tolerances realistic?
Can fixtures locate the part reliably?
Can automated equipment reach the required features?
Can workers assemble it without excessive manual adjustment?
Can defects be detected efficiently?
Can the process remain stable when volume increases?
A design can be physically manufacturable and still be a poor production design if it creates excessive inspection, rework, scrap or specialised manual work.
Electronics Makes DFM Easy to See
IPC describes DFM as a necessary but frequently neglected or skipped step in product development.
Its DFM Profiles connect design requirements with multiple performance classes and producibility levels, ranging from relatively straightforward electronics to high-density and high-reliability applications.
That matters because there is no single “best” manufacturing rule for every product.
A simple commercial device does not necessarily need the same architecture as equipment where very high continued performance is required.
The requirement has to come first.
Otherwise teams can overengineer a simple product or under-design a critical one.
Manufacturing, Assembly and Testing Are Different Questions
IPC's DFX framework goes beyond manufacturing alone.
IPC-2231A includes Design for Manufacturing, fabrication, assembly, testability, cost, reliability, environment and reuse. The purpose is to create disciplined design review around attributes that affect the real production of electronics hardware.
A board may be fabricatable but difficult to assemble.
It may assemble successfully but be difficult to test.
It may pass functional testing yet be too sensitive to manufacturing variation.
IPC therefore also distinguishes DFM, Design for Test and Design for Assembly as related but separate disciplines.
“Manufacturable” is not one checkbox.
It is a chain of capabilities.
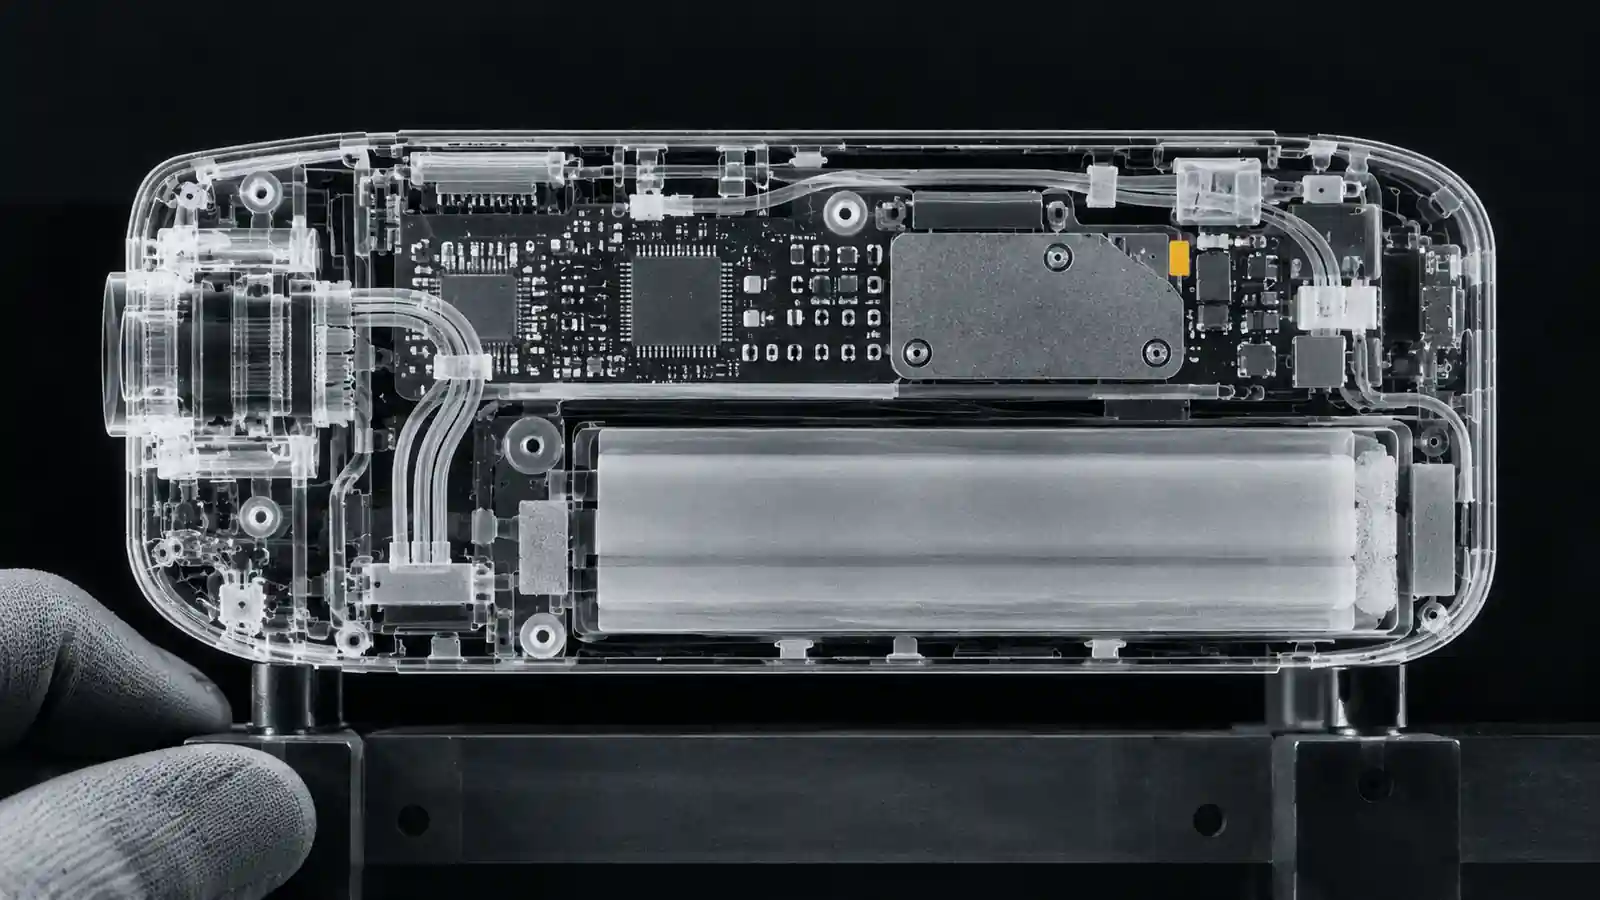
Testability Has to Be Designed
Testing is often treated as something that happens when a product is complete.
Design decisions determine how practical that testing will be.
Can critical signals be accessed?
Are test points reachable?
Can a fixture connect consistently?
Do hidden assemblies prevent inspection?
Will basic fault diagnosis require the entire device to be disassembled?
Thinking about those questions early can prevent expensive testing problems later.
A product should be designed not only to function.
It should also be designed so failures can be found.
Component Choice Is Also a Manufacturing Decision
An engineer may choose a component because its technical performance is excellent.
Manufacturing adds further questions.
Can it be sourced consistently?
Does its package fit the manufacturer's assembly capability?
Does placement create adequate process margin?
Can the part be inspected and reworked?
Will its tolerance interact with surrounding parts?
Does the thermal design remain practical?
ASME explicitly includes availability, retooling needs, tolerances and compliance/testing among DFM considerations.
A Bill of Materials is therefore not simply an electrical list.
It is part of production strategy.
The Cheapest Component Does Not Necessarily Create the Cheapest Product
DFM is sometimes misunderstood as a programme to make every component cheaper.
Total manufacturing cost does not work that way.
A cheaper connector may increase assembly time.
A smaller PCB may save material while making fabrication substantially harder.
An unnecessarily tight tolerance can increase scrap.
Removing a test point may save space while making failure diagnosis slower.
The relevant question is total system cost and performance.
ASME's formulation is useful: manufacture economically without sacrificing function and performance.
Manufacturability is not an excuse to weaken the product.
It is a way to understand the trade-offs before they become expensive.
Reliability Must Match the Application
IPC's design profiles vary by performance requirement and producibility because electronic products operate under very different expectations.
Consumer electronics, industrial controls and highly critical equipment do not necessarily need identical reliability architectures.
The product requirement should therefore guide manufacturing decisions.
Overengineering can make a straightforward product unnecessarily expensive.
Underengineering a critical product can create far more serious consequences.
DFM works best when production choices remain tied to intended use.
Indonesia's Opportunity Is More Than Machine Capacity
The Ministry of Industry's 16 October release also shows that domestic electronics development is not only a question of buying equipment.
It identifies challenges around consistent quality, delivery, production scale, longer-term contracts, financing and standards such as ISO and IPC.
Industrial upgrading therefore works in both directions.
Manufacturers need stronger capability.
Product owners and designers also need designs compatible with available processes.
When local manufacturing enters only after design freeze, much of the opportunity to optimise the product around those capabilities has already disappeared.
Early collaboration creates more options.
Freeze the Design After Manufacturing Knowledge Arrives
Design freeze is necessary.
Without it, sourcing, tooling and production planning cannot stabilise.
The question is when the freeze occurs.
If a design is locked before manufacturing, assembly, testing, quality and suppliers have contributed, the company may simply be freezing untested assumptions.
IPC's design initiative emphasises collaboration across OEMs, PCB manufacturers, electronics manufacturing services, packaging specialists and design-tool ecosystems.
A strong design freeze is therefore the result of integration.
It is not evidence that engineering has stopped listening to manufacturing.
From Requirement to Design Release
As a GATICORP editorial framework:
Requirement → Architecture → Component Choice → Manufacturability Review → Prototype → Assembly & Test → Production Feedback → Design Release
The framework creates a feedback loop rather than a handoff.
Manufacturing knowledge returns to design while changes are still manageable.
Prototype and test results challenge assumptions.
Production feedback exposes yield, variation and assembly problems.
Only then does release turn the design into a controlled manufacturing configuration.
This is not an IPC standard.
It is a business-oriented way to place manufacturing inside product development.
The Factory Is Not Where Finished Designs Go to Be Fixed
CAD can look perfect.
Simulation can work.
An engineering prototype can function.
Commercial products still have to survive another reality:
machines, materials, tolerance, operators, fixtures, assembly, testing, yield, rework and volume.
Those are not external annoyances imposed on design.
They are part of the world in which the design must operate.
Manufacturing should therefore not become the place where a supposedly finished design is finally tested by reality.
Manufacturing knowledge should arrive while dimensions, materials, components and architecture are still cheap enough to change.
A product is not ready merely because its design file is complete.
It is ready when it can be made consistently in the real world.
- Indonesia Ministry of Industry, 16 October 2026 — Global Electronics Market to Exceed USD1 Trillion. Used for the current Indonesian context, existing SME component capabilities and the challenges around quality, scale, financing, contracts and standards.
- IPC — Design for Manufacturing Profiles. Used for DFM's role in product development and its performance-class/producibility-level structure.
- IPC-2231A — DFX Guidelines. Used for DFX coverage of manufacturing, fabrication, assembly, testability, cost, reliability, environment and reuse.
- IPC — DFM, DFT and DFA. Used to distinguish manufacturability, testability and assembly considerations.
- ASME — Design for Manufacturing. Used for the principle of economical manufacturing without sacrificing functionality and performance and for the role of materials, availability, tooling, tolerances, testing and manufacturing collaboration.
- NIST — Integrating Process Planning with Conceptual Design. Used for the value of evaluating manufacturability and manufacturing cost during early product development.
- Editorial note: electronics provides the current hook, but Design for Manufacturing applies far more broadly, with different methods and standards across product and process categories. Requirement → Architecture → Component Choice → Manufacturability Review → Prototype → Assembly & Test → Production Feedback → Design Release is a GATICORP editorial framework.
Published: October 23, 2026